3D print spaghetti: causes, recovery and prevention
3D print spaghetti is the tangle of loose filament you get when a part breaks free, collapses or gets knocked over mid-print and the printer keeps extruding into thin air. Almost every case traces back to bed adhesion, a failed support or a problem in the sliced file, and most can be prevented with a good first layer and automatic failure detection.
- Stop the print from the screen or app, and keep your hands away from moving parts.
- Look at what broke: is the part off the bed, a support snapped, or the part still stuck with the tangle on top?
- Clear strings with flush cutters or tweezers, and check for a blob of plastic around the nozzle.
- Fix the cause, usually by cleaning the plate and re-checking the first layer.
- Turn on failure detection if your printer or print host has it.
What causes 3D print spaghetti?
The printer has no idea the part has gone. It follows the G-code, so if the object underneath moves, every new layer lands on nothing. Prusa lists three main reasons: the object detaches from the bed, the object collapses, or there's an error in the model or sliced file.
| What you find | Likely cause | Fix |
|---|---|---|
| The part is loose on the bed or stuck to the nozzle | Bed adhesion failed, often from a dirty plate, wrong bed temperature or warped corners | First layer not sticking, warping |
| Part still stuck, tangle starts at an overhang | A support broke away or was too sparse | Stronger supports with a wider base; see the supports guide |
| Tall, thin part snapped or fell over | Too little footprint, or the nozzle hit a curled edge | Add a brim, orient for a wider base, enable Z-hop |
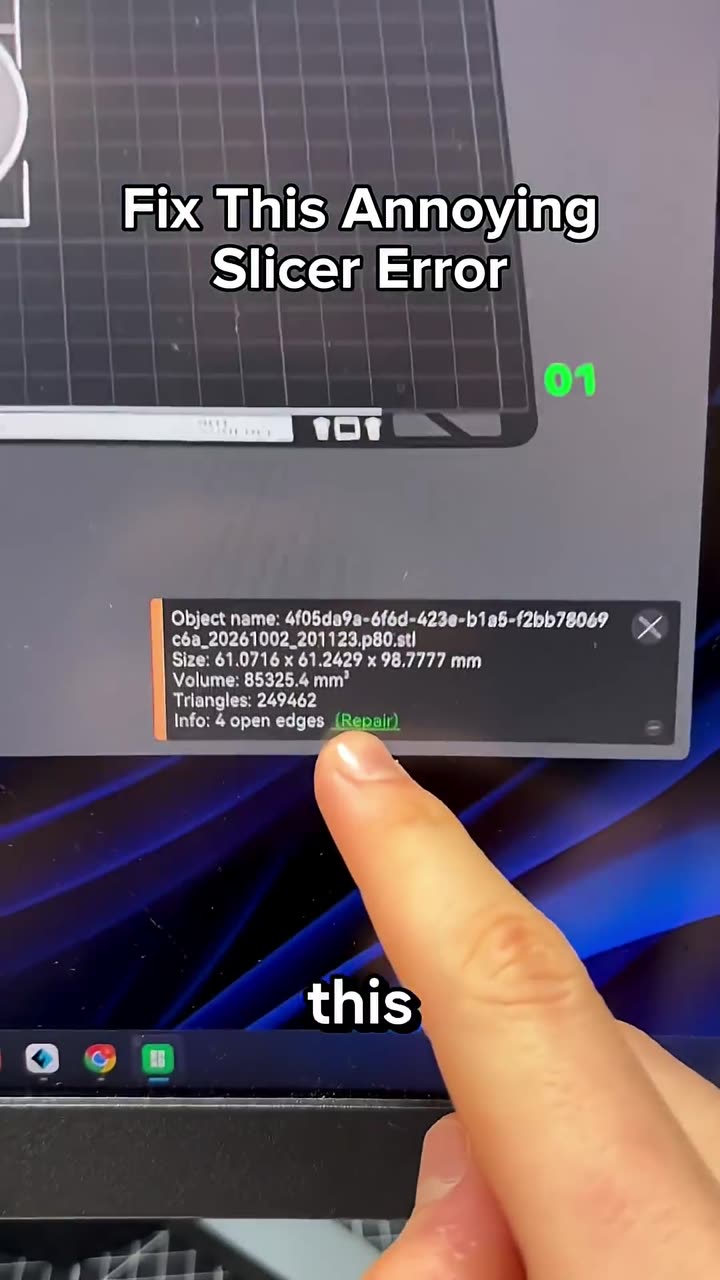
| Tangle starts at the same height every time | Model or slicing error: a floating island, missing layers or broken geometry | Check the preview; repair the mesh |
| Layers continue but offset sideways, then fail | A big layer shift moved the print area | Layer shifting |
| Toolhead moving but nothing coming out | Extrusion stopped (clog, heat creep, tangled spool) | Clogged nozzle, heat creep |
If the tangle always starts at the same height, open the sliced file in a G-code viewer before blaming the printer. Floating sections show up as lines starting in mid-air. Broken meshes can be fixed with PrintPal's mesh repair tool before you re-slice.
Free PrintPal toolG-code ViewerStep through layers to find floating islands before you printOpen toolYou find spaghetti, but the main part is still stuck firmly to the bed. The tangle starts right where a thin support tower held up an overhang, and the tower has snapped off. What failed?
The part stayed put, so adhesion was fine. The overhang lost its support when the tower broke, and every layer above it printed into air. Give supports a wider base or more density, or reorient the part to need less support.
How to clean up spaghetti safely
- Cancel the print. Wait until the axes stop before reaching in.
- Check the hotend. If plastic has built up around the nozzle and heater block, skip to removing an extruder blob. If it's just strings, let the hotend cool.
- Remove strings with flush cutters or tweezers, not fingers. Don't yank strings wrapped around wires or fans; cut them free.
- Clear the bed. Remove the failed part, then clean the plate. Bambu Lab recommends washing plates with warm water and detergent to restore adhesion.
- Inspect for damage: strings in the hotend or part cooling fan, plastic on cables, and gouges in the build surface.
- Find the cause before reprinting, using the table above.
How to remove an extruder blob
An extruder blob, sometimes called the blob of doom, is a lump of plastic that builds up around the hotend. Prusa notes it often happens early in a print, when the first layer detaches and sticks to the hot nozzle while it keeps extruding. The thermistor and heater cartridge wires are often trapped inside, so go slowly.
Hot, sharp and electrical. The hotend can be over 250 °C. Wear eye protection, use pliers rather than fingers, and switch the printer off before you start pulling plastic, because tugging on damaged heater or thermistor wires while powered can cause a short.
- Heat the nozzle about 30 °C above the blob's print temperature. Prusa's examples are 250 °C for PLA and 280 °C for PETG or ABS.
- Wait at least 5 minutes for the heat to soak through the blob.
- Turn the printer off, then pull the softened plastic away with pliers, a little at a time. Small blobs may drop off on their own.
- Watch the wires. Work around the thermistor and heater leads, not through them.
- Finish with a brass brush to clear what's left.
- If the printer shows MINTEMP or a heater error, the wiring is probably already damaged. Use a heat gun carefully instead, and replace the damaged parts before printing again.
A silicone sock on the heater block won't prevent a blob, but it makes one much easier to remove.
Spaghetti detection: AI cameras and other checks
Automatic detection won't stop a failure from starting, but it pauses the print before a small mess becomes a big one.
- Built-in AI camera detection. Several printers run a failure-detection model on images from their camera. Examples include Bambu Lab's X1 series, which runs it on the printer itself using the chamber camera, newer Bambu models such as the H2D and P2S, and Creality's K1C, K1 Max and K2 Plus. You can usually set the sensitivity and choose whether it pauses or just alerts you.
- Add-on services for other printers. Tools such as Obico (for OctoPrint and Klipper, cloud or self-hosted) and SimplyPrint watch a webcam feed and pause the print when they spot a failure.
- Non-camera checks. Some newer printers also detect air printing or a tangled spool from the extruder motor. A filament runout sensor won't spot spaghetti, but it stops one cause of failed prints.
Detection isn't foolproof. Bambu Lab warns of false positives and missed detections, especially with black or dark filament, and its detector needs the chamber light on. Treat detection as a safety net, not a reason to skip the first-layer check.
First-layer checks
Most spaghetti starts with a weak first layer, so this is where watching pays off. Some printers inspect it automatically, for example first-layer inspection on Bambu Lab X1 printers and first-layer detection on some Creality K-series models. On any printer, a quick look at the first two layers through a camera or in person catches most adhesion problems.
Cancel one object and save the rest of the plate
If one part on a full plate fails, you don't have to lose the whole print. Cancel only that object and the rest keeps printing.
- Prusa: Tune → Cancel Object on the printer, or from Prusa Connect. Needs a file sliced in a recent PrusaSlicer.
- Bambu Lab: Skip Objects from the printer, Bambu Studio or Bambu Handy.
- Klipper: enable
[exclude_object], label objects in the slicer (or let Moonraker process the file), then cancel from Mainsail or Fluidd. - Marlin:
M486, if the firmware was built withCANCEL_OBJECTS.
[exclude_object]

EXCLUDE_OBJECT NAME=part_2
M486 P1 ; cancel the object with index 1How to prevent spaghetti
- Clean the build plate before each print; fingerprints are a common adhesion killer.
- Use the right bed temperature for the material, such as 55–65 °C for PLA and 70–85 °C for PETG.
- Add a brim to small, tall or sharp-cornered parts.
- Give supports a solid base and enough contact with the overhang.
- Check the sliced preview for floating islands and unsupported starts.
- Enable Z-hop if curled edges or overhangs could catch the nozzle.
- Watch the first layers, then turn on detection or a camera.
- Keep a smoke alarm near the printer; the 3D printing safety guide covers the rest.
Frequently asked questions
What causes spaghetti in 3D printing?
Spaghetti happens when the printer keeps extruding but the part underneath has moved or gone. The usual causes are the part detaching from the bed, a support or thin section breaking off, the nozzle knocking the part over, or a problem in the model or sliced file.
How do I stop my 3D prints turning into spaghetti?
Get a clean, well-stuck first layer, use a brim on small or tall parts, give supports a solid base, and check the sliced preview for floating sections. Then turn on any failure detection your printer offers and check the first few layers yourself.
Which 3D printers have AI spaghetti detection?
Several camera-equipped printers include it, such as Bambu Lab's X1 series and newer H2 and P2S models and some Creality K-series printers. For other printers, add-on services such as Obico and SimplyPrint can watch a webcam feed. Detection still misses some failures, especially with dark filament.
Can I save a print when one part fails?
On a plate with several objects, yes: cancel just the failed object and let the rest finish. Prusa's Cancel Object, Bambu Lab's Skip Objects, Klipper's exclude_object and Marlin's M486 all do this when the file was sliced with object labels.
Is it safe to leave a 3D printer unattended?
Manufacturers such as Prusa advise against leaving a printer unattended while it is on. If you do step away, keep thermal protection enabled, use failure detection or a camera, keep the area clear of flammables and fit a smoke alarm nearby.
Related articles
Sources & further reading
- Prusa Knowledge Base — Spaghetti monster
- Prusa Knowledge Base — Extruder blob
- Bambu Lab Wiki — Spaghetti detection
- Prusa Knowledge Base — Cancel Object
- Klipper Docs — Exclude objects
Tools for thisAll tools
Watch it doneVideo library
Thanks! We read every note and use them to decide what to update next.